How to Choose Zirconia Tubes for Your Application?
Choosing Zirconia Tubes starts with the job they must perform, not a catalogue label. Will the tube face thermal cycling, corrosive media, electrical insulation demands, or repeated mechanical contact? Those conditions determine whether stabilized zirconia, dimensions, and surface finish are suitable. Small details matter: a tight bore, a rough edge, or a sudden temperature change can turn a promising specification into an early failure.
The market context is growing. Grand View Research estimated the global zirconia market at about US$1.46 billion in 2022 and projected a 5.5% compound annual growth rate from 2023 to 2030. That figure covers zirconia broadly, not tubes alone. It signals expanding material use, but it cannot tell you which grade belongs in your assembly. In their landmark Nature paper, materials researchers Robert C. Garvie, R. H. Hannink, and R. T. Pascoe used the phrase “ceramic steel” for transformation-toughened zirconia. Memorable, yes. Not a design guarantee. Tube performance still depends on composition, geometry, manufacturing quality, and operating conditions.
A sound choice compares these factors against actual service data: peak temperature, chemical exposure, load, and required lifetime. Ask suppliers for grade-specific property sheets and tolerances, then verify critical dimensions on received parts. Published values are useful, but test results from your own process are better. I would not treat a single hardness or temperature rating as decisive; that shortcut is tempting, and sometimes wrong. This guide explains how to assess Zirconia Tubes with practical criteria, clear trade-offs, and questions worth asking before ordering.
Define the Operating Conditions and Performance Requirements
Start with the tube’s real operating environment, not just its nominal temperature. Record the minimum and maximum temperatures, heating rate, hold time, and number of cycles. A furnace that reaches 1,000°C slowly presents different stresses from one that heats rapidly. Note the surrounding atmosphere, too: oxygen, moisture, vacuum, or reactive gases can affect material performance.
Then define the mechanical and chemical demands. Will the tube support a sensor, carry fluid, or sit under vibration? Specify internal pressure, bending loads, contact points, and exposure to corrosive substances. Include the required inner diameter, outer diameter, length, and dimensional tolerances. Small details matter. A tight fit may crack during thermal expansion, while excess clearance can weaken support.
Set measurable performance targets, such as electrical insulation, thermal conductivity, purity, or service life. These depend on the application, so avoid choosing a grade by temperature rating alone. If failure would stop a process, consider how the tube will be inspected and replaced. A tidy specification can still miss an unusual startup cycle; review real operating records where possible. If conditions are uncertain, test a sample under representative heat and load before finalizing the design.
Match Zirconia Grade to Required Material Properties
How to Choose Zirconia Tubes for Your Application?
Match Zirconia Grade to Required Material Properties
Zirconia grades differ in strength, toughness, thermal behavior, and resistance to wear or chemical attack. These properties depend on the formulation and stabilizer content, so “zirconia” alone is not a sufficient specification. Start with the tube’s working conditions: operating temperature, thermal cycling, applied load, and contact with process chemicals. Then compare those needs with grade-specific technical data. Small details matter. A tube used near a furnace element may face sharp temperature changes, while one in a pump assembly may need better wear resistance. It is easy to focus only on peak temperature, but that can overlook mechanical stress or chemical exposure.
Consider the tube’s dimensions and manufacturing tolerances as well. Wall thickness can affect heat transfer and resistance to handling damage, while tight dimensional requirements may limit suitable production methods. Ask for data on the finished component, not just general material properties. When conditions are unusual, a small trial under realistic operating conditions can reveal issues that a datasheet cannot. Be cautious about assuming one grade will perform equally well across different setups.
Tips: List the expected temperature range, load, and chemical exposure before selecting a grade. Confirm test conditions behind reported values, and review compatibility with a qualified materials specialist. If the application changes, reassess the choice.
Select Tube Dimensions, Shape, and Tolerances
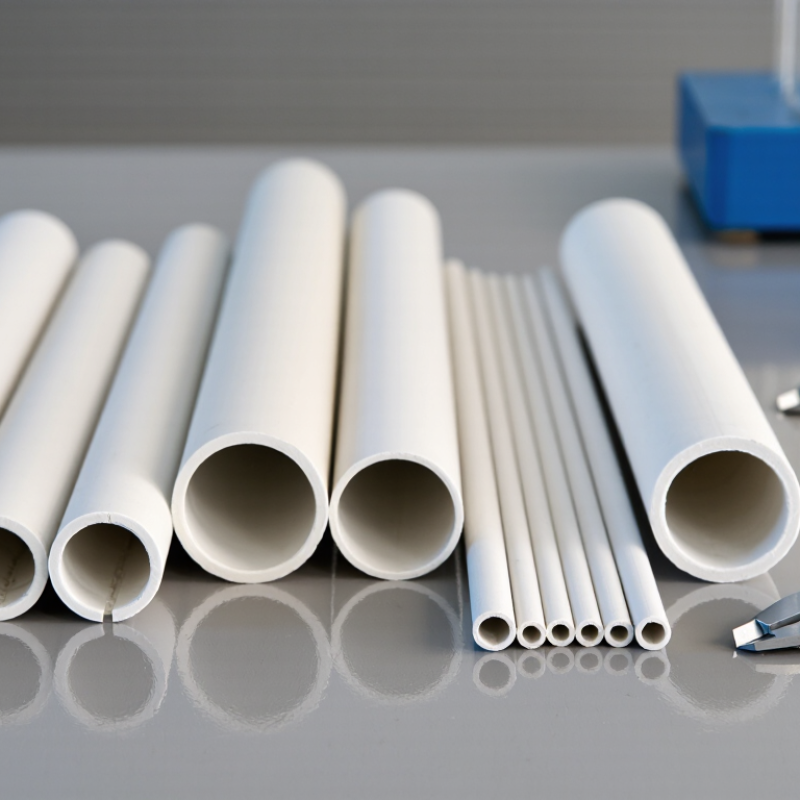
Start with the working space, not a catalogue size. Measure the tube’s outer diameter, inner diameter, wall thickness, and usable length against the assembly drawing. A tube with a 10 mm outer diameter and a 2 mm wall has a 6 mm bore, but manufacturing variation can affect that opening. Small gaps matter. Check how the tube will be held, heated, and loaded, since each condition can change the fit you need.
Choose a shape that suits the job. Round tubes often fit rotating or fluid-handling assemblies, while square or rectangular sections can resist movement in a fixed mount. Consider the ends, too: a cut edge, chamfer, or stepped feature may determine whether the tube seats cleanly. Zirconia is hard and brittle, so avoid assuming it will tolerate forced installation or sharp impact. Fit is everything. Sometimes, a simpler geometry is more reliable.
Set tolerances around function rather than habit. Specify tighter limits only where a mating part, seal, or alignment requires them; overly strict tolerances can increase machining difficulty and cost. State whether dimensions refer to the finished part, and identify critical measurements on the drawing. If operating temperature matters, account for expansion in the surrounding components as well. A prototype can reveal issues a drawing misses, though one sample is not proof of consistent production. Recheck the dimensions that affect assembly.
How to Choose Zirconia Tubes for Your Application? - Select Tube Dimensions, Shape, and Tolerances
Use the examples below as a starting point. Dimensions and achievable tolerances depend on zirconia grade, forming and finishing processes, tube length, and inspection method; confirm critical requirements with the manufacturer.
| Application or priority |
Suitable tube shape |
Illustrative dimensions (mm) |
Indicative tolerance targets |
Selection notes |
| Small fluid or gas passage |
Straight capillary tube |
OD 2.0; ID 1.0; length 50 |
OD/ID: about ±0.05–0.10; length: about ±0.2–0.5 |
Specify the minimum bore and flow requirement. A small ID may be more difficult to measure and finish consistently. |
| Wear-resistant sleeve or guide |
Straight, open-ended tube |
OD 10.0; ID 6.0; length 40 |
OD/ID: about ±0.05–0.10; length: about ±0.2–0.5 |
For a close-fitting shaft, define the required clearance and identify which surface is functionally critical. Consider specifying surface finish where contact or sliding occurs. |
| Protective sheath for a probe or sensor |
Closed-end tube |
OD 8.0; ID 5.0; body length 100; closed-end thickness 1.5 |
OD/ID: about ±0.10; length: about ±0.5–1.0; end thickness: confirm by drawing |
State whether the closed end is flat or rounded and specify the usable internal depth. Check thermal shock, chemical exposure, and installation loads for the application. |
| Thin-wall, lightweight component |
Thin-wall straight tube |
OD 6.0; ID 5.0; nominal wall 0.5; length 30 |
OD/ID: about ±0.10; wall: define minimum; length: about ±0.2–0.5 |
Thin walls are more sensitive to handling and processing variation. Specify minimum wall thickness and, if important, wall uniformity around the circumference. |
| Positioning or assembly with a locating feature |
Stepped tube or tube with a shoulder |
Main OD 12.0; shoulder OD 14.0; ID 7.0; length 60 |
Critical diameters: set on drawing; shoulder location: about ±0.2–0.5 as a starting target |
Dimension the shoulder from a clear datum. Tight fits or precise shoulder positions may require additional grinding and inspection. |
| Flow outlet or directional delivery |
Tube with a bevel or angled end |
OD 6.0; ID 3.0; length 40; bevel 30° |
OD/ID: about ±0.10; bevel angle and end condition: specify on drawing |
Define the angle, orientation, and acceptable edge condition. For a sealing or mating face, specify flatness or face geometry separately. |
Dimensions and tolerances to define on a drawing
- Specify outside diameter (OD), inside diameter (ID), overall length, and minimum wall thickness; state units and any critical dimensions.
- For fit or alignment, consider adding concentricity or total runout, straightness, and end-face squareness requirements rather than relying on OD and ID tolerances alone.
- Use tighter tolerances only where function requires them. Precision grinding may improve dimensional control but can increase cost and lead time.
- Indicative ranges in this table are planning examples, not guaranteed limits or a universal standard. Confirm tolerances, inspection capability, material grade, and finished-part condition before release.
Evaluate Manufacturing Quality and Supplier Specifications
When comparing zirconia tubes, inspect evidence behind the specification, not just the headline strength. A review of zirconia biomaterials reports flexural strength around 900–1,200 MPa for common 3Y-TZP ceramics, while noting that composition and processing affect results (Chevalier, Biomaterials, 2006). That range is useful context, not a tube guarantee. Ask for the test method, sample geometry, and batch-specific results. ASTM C1161 describes flexural-strength testing for advanced ceramics and can help clarify how suppliers generated their figures.
Check the drawing against measurable controls: outside and inside diameter, wall thickness, straightness, concentricity, and end-face squareness. For a tube used in a close-fitting assembly, request actual tolerance data and an inspection report from the production lot. Look for density, open porosity, surface-finish limits, and evidence of visual or dimensional inspection. Ask how defects are recorded. Small chips near an edge can matter.
Supplier documentation should identify zirconia grade, stabilizer content, firing process, and traceability method. Request thermal-shock or chemical-resistance data when service conditions demand it, rather than accepting a generic claim. ISO 13356 covers specified zirconia material for surgical implants, so it may inform material discussions but does not qualify every industrial tube. I would not treat a polished datasheet as proof. Sometimes the missing detail is the real issue.